High-Containment Capsule Filling: NJP-800A-HC Guide
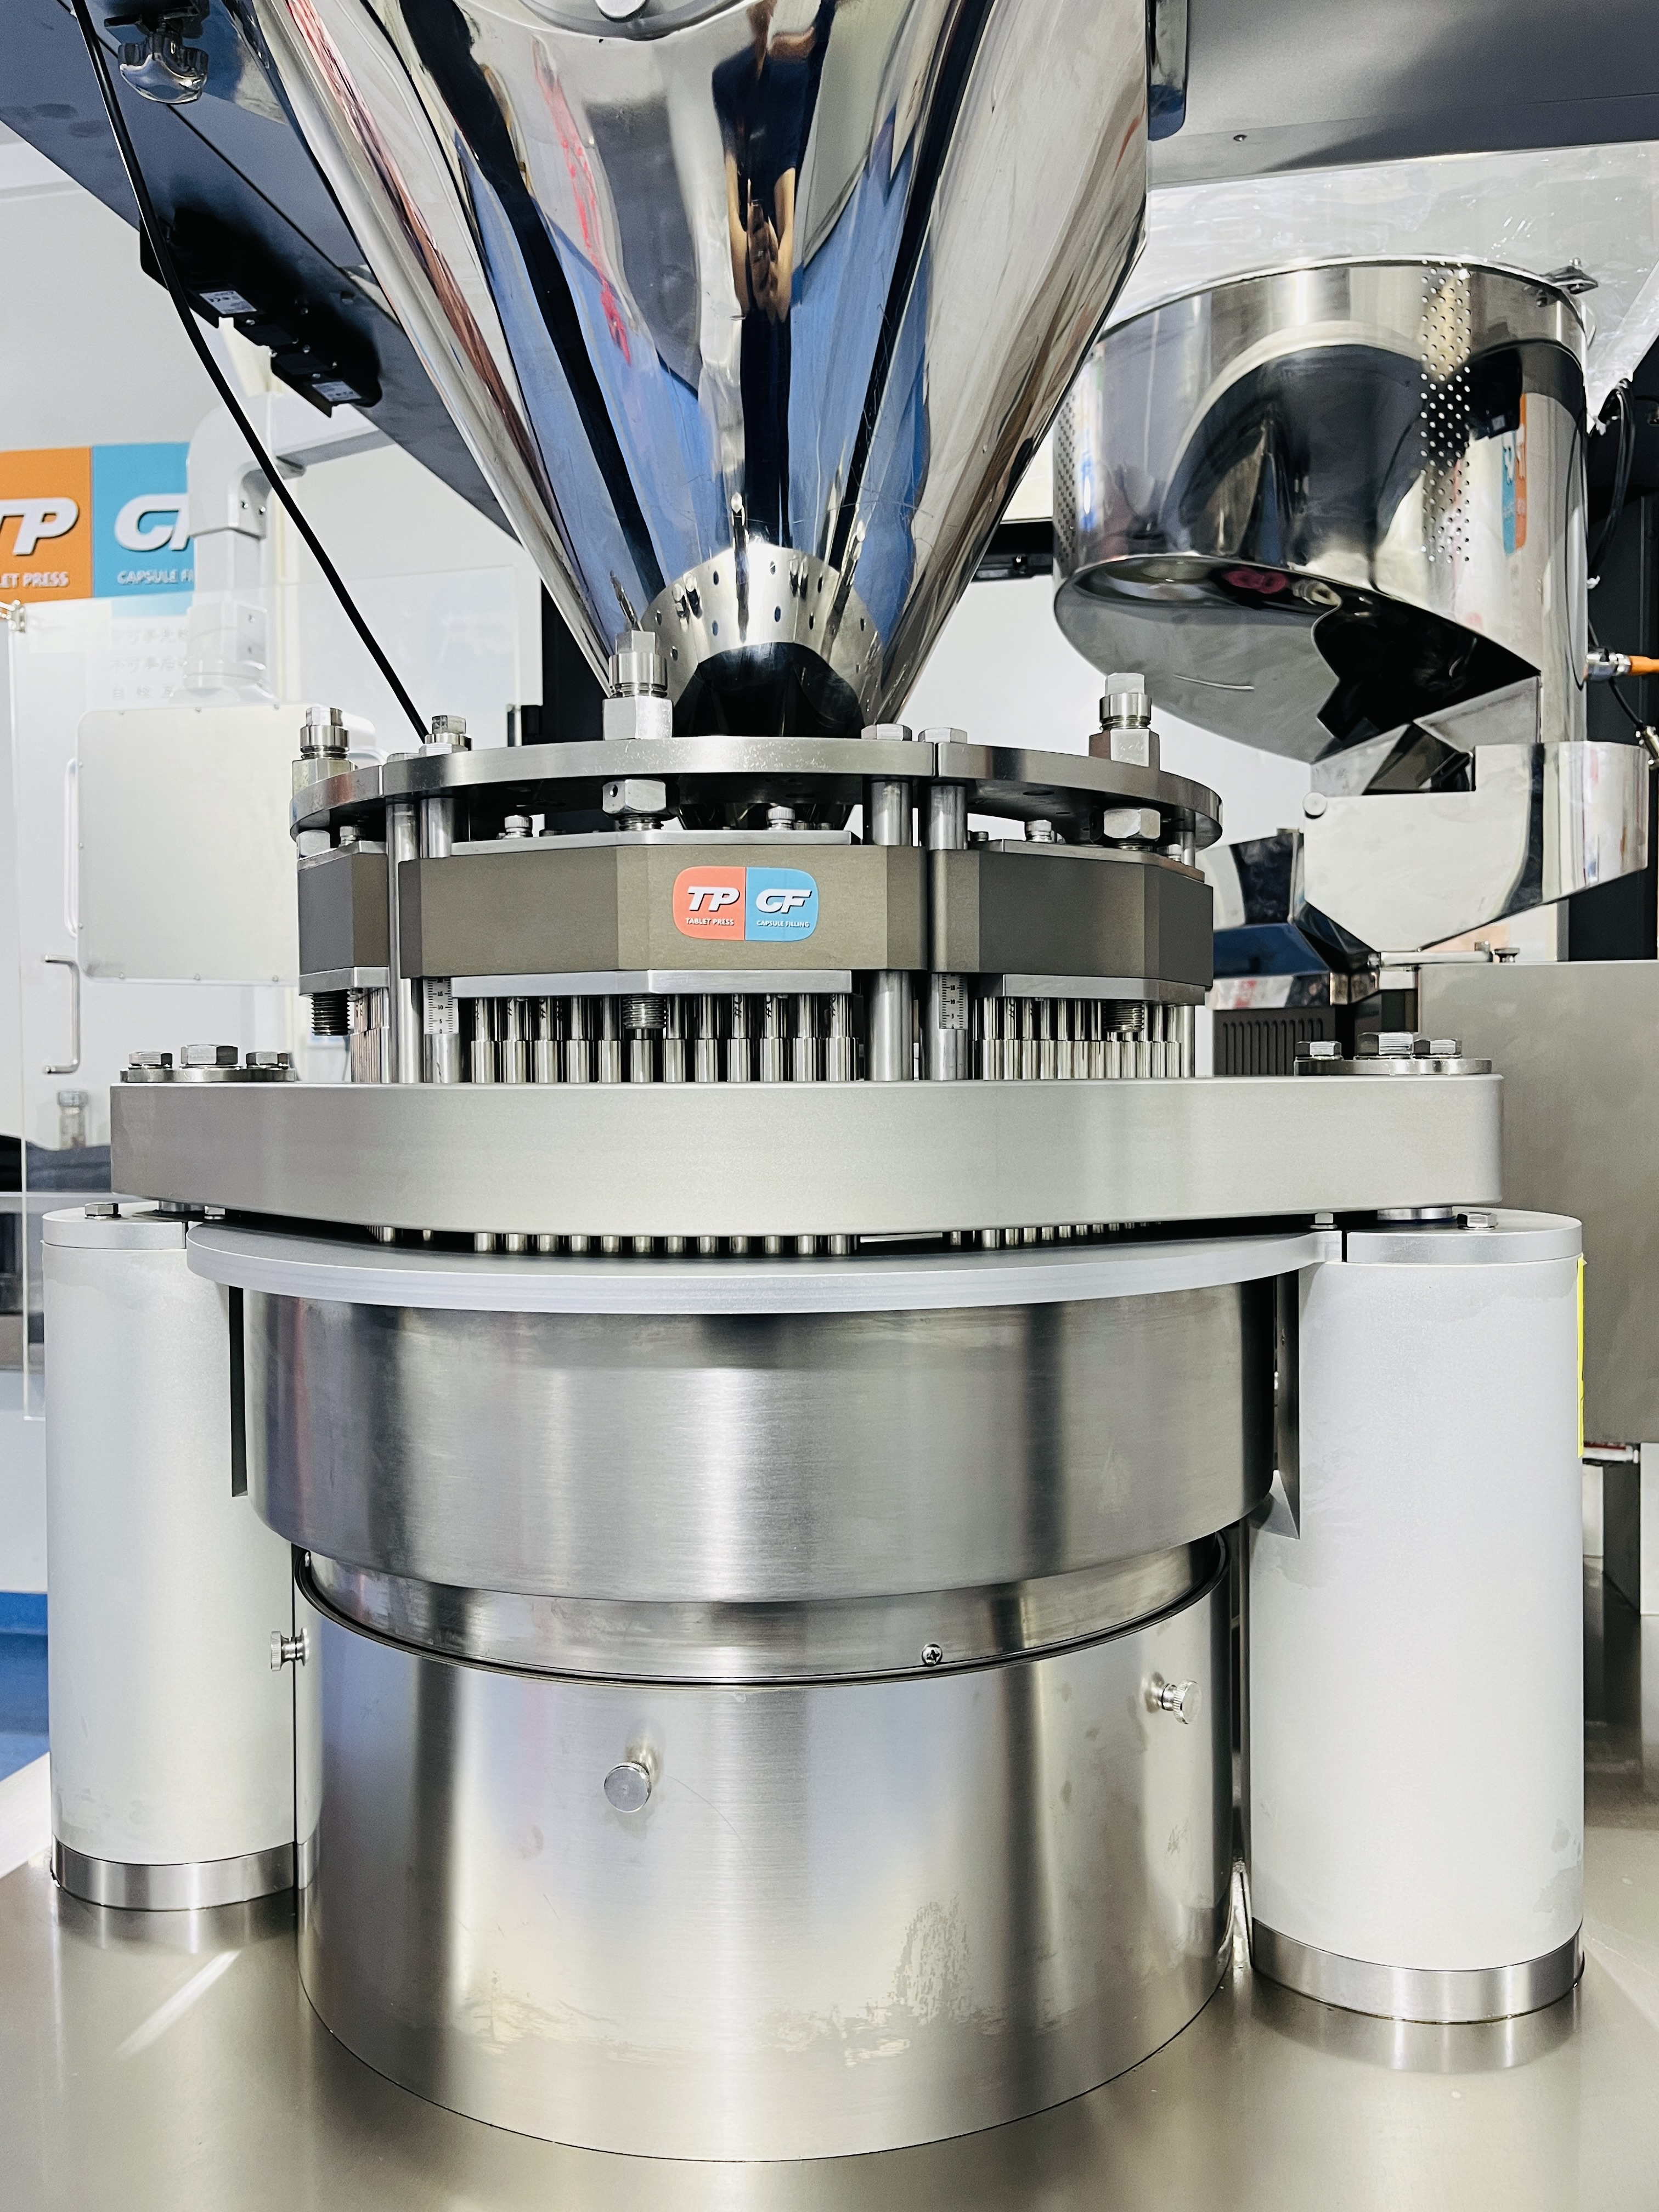
Potent compounds change what a capsule filling machine has to be. Once the active ingredient is assigned to occupational exposure band 4 (OEB4), throughput stops being the only benchmark and containment becomes the design constraint: the machine must keep powder inside the process, not merely move it quickly. The NJP-800A-HC is TPCF's OEB4 high-containment automatic hard capsule filling machine, rated for a maximum output of 800 capsules per minute, configured with 7 die bores, specified at ±3% dosing accuracy, and compatible with capsule sizes 00# to 5# as well as safety capsules A to E. Its product and capsule contact parts are stainless steel, the filling process runs inside a fully enclosed chamber, and the design is GMP-compliant.
Shanghai Tablet Press Mechanical Components Co., Ltd. (TPCF) is a Shanghai-based pharmaceutical machinery manufacturer producing tablet presses, tablet press tooling and capsule filling machines, operating a 15,000 m² factory in Songjiang District and exporting roughly half of its output. This guide explains what the NJP-800A-HC is, how containment is engineered into it, where containment legitimately outweighs raw output, and how to qualify the machine before a purchase decision.
Why Potent Compounds Break Conventional Capsule Filling
Containment problems in capsule filling are created at the dosing and closing stations, where powder is metered into the capsule body and the cap is joined at speed. Those repeated mechanical movements push fine particles into the air. On an open-construction machine, that dust is managed by room air handling, operator technique and personal protective equipment — a combination that depends on human discipline as much as on engineering.
The consequences of under-controlled dust are commercial as well as clinical: cross-contamination risk in a shared suite, extended cleaning cycles, failed cleaning verification, and audit findings on containment and documentation. For an OEB4 product, those consequences are the reason containment is assessed before output is even discussed.
- Capsule feeding and opening: empty capsules separate at high speed and generate fine shell debris.
- Powder dosing: the highest dust-generation point on the machine, and the point closest to the operator.
- Capsule closing and ejection: residual powder on the outside of the capsule transfers to chutes and containers.
- Cleaning and changeover: the moment when contained dust is most likely to be re-released.
Evaluation-stage rule of thumb: containment is not a feature bolted onto a capsule filling machine; it is the geometry of the machine. If the enclosure, the dust path and the cleaning route were not designed together, the nameplate output figure has little meaning for a potent product.
Industry Background: Regulation, Containment Bands and Market Signals
The regulatory frame
Pharmaceutical manufacturers supplying the United States must comply with 21 CFR Part 211, the Current Good Manufacturing Practice regulation for finished pharmaceuticals, published by the U.S. Food and Drug Administration. Other regulated markets apply their own GMP frameworks, but the practical common denominator is the same: documented control of cross-contamination, documented cleaning and documented equipment qualification. A high-containment capsule filling machine is therefore evaluated as part of a validation package, not as a stand-alone purchase.
Occupational exposure bands
Occupational exposure bands classify compounds by hazard. OEB4 describes a highly potent compound that requires a high level of containment. Band definitions and the exposure limits behind them are set by each manufacturer's toxicology and EHS functions rather than by one global standard, so a supplier's OEB4 claim should be read as the containment tier the design was engineered for — and then verified against your own band assignment and your own acceptance criteria.
What the market numbers do and do not tell you
Commercial research indicates that automatic capsule filling machines accounted for over 65% of the total capsule filling machine market in 2024, reflecting the dominance of automated production in pharmaceutical manufacturing. Absolute market values are far less stable: one commercial estimate places the global market at USD 0.9 billion in 2024, while another places it at USD 238.0 million in 2025. The gap reflects different product scopes rather than measurement error, and the two figures should not be averaged or reconciled without a methodology review.
What to use for planning: the segment signal — automatic machines dominate commercial capsule production — is stable and useful. The absolute market value is not. Base a capacity decision on your own batch schedule, not on a market-sizing figure.
The NJP-800A-HC in Detail
Fully enclosed containment chamber
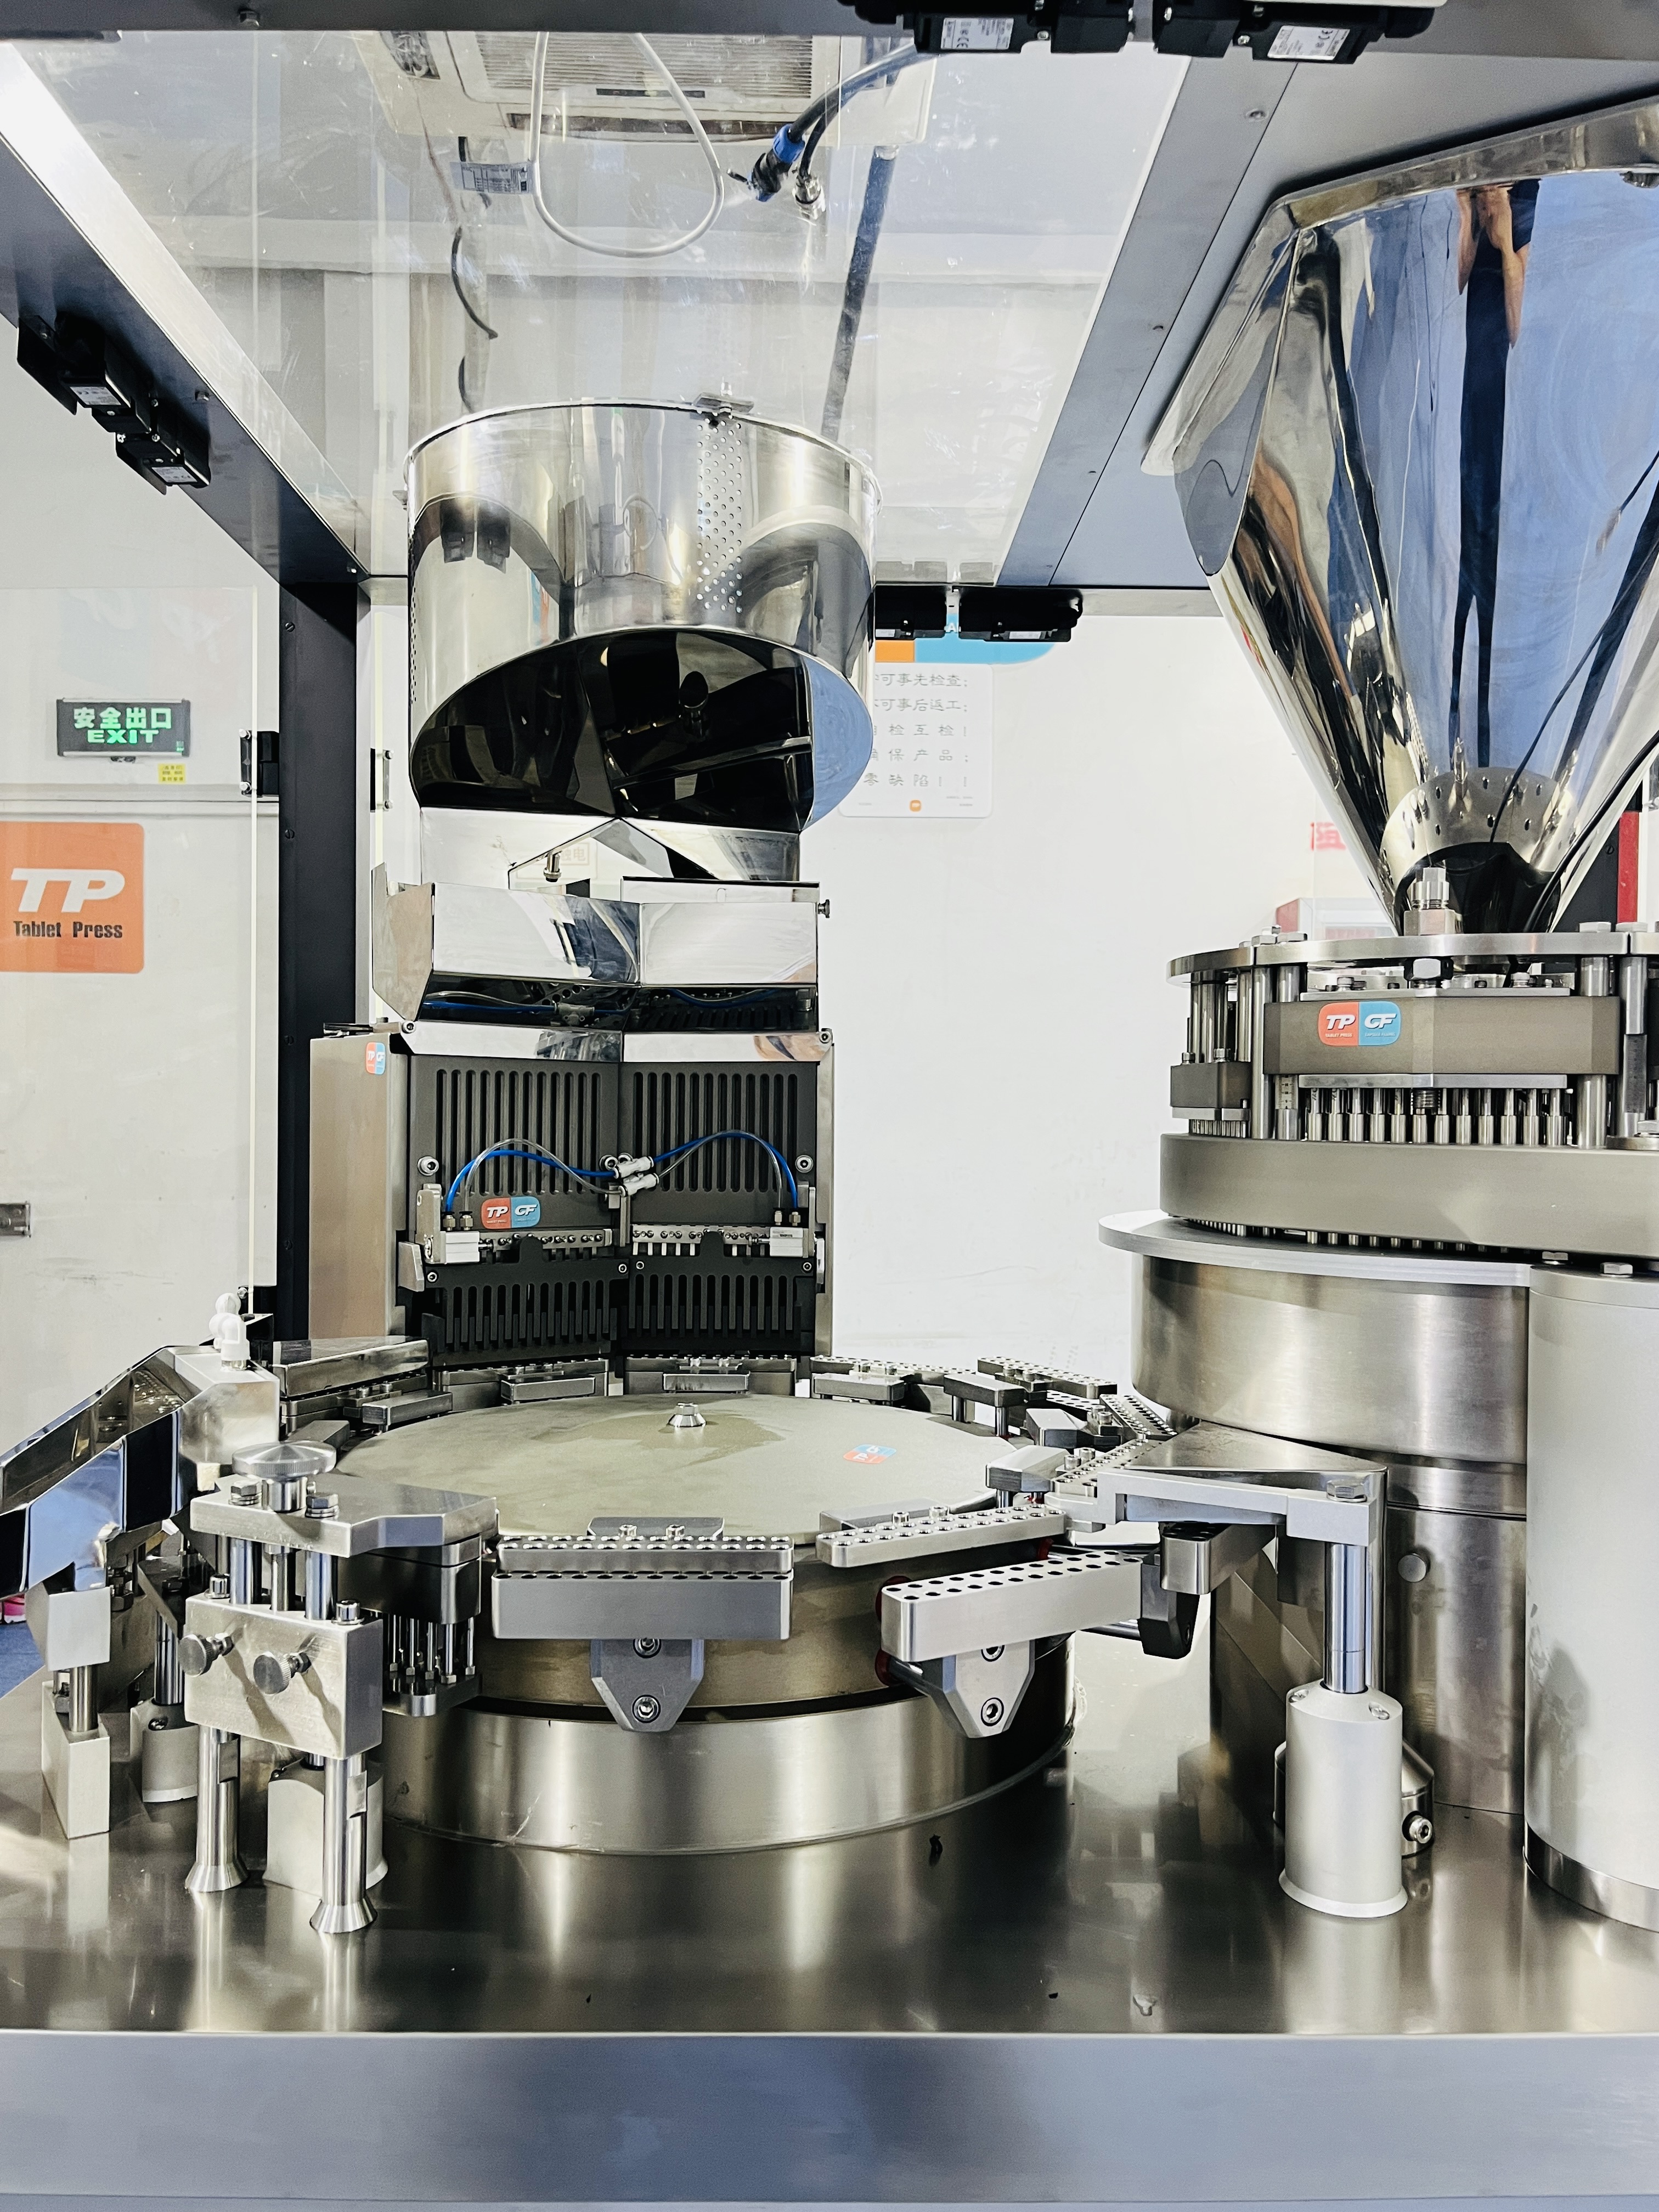
The NJP-800A-HC places the dosing, capsule handling and closing stations inside a fully enclosed chamber, so the dust-generating area is physically separated from the operating room. This is the primary engineering control for a potent product: the enclosure captures particles at the point of generation, and the operator interacts with the process through the machine interface and cleaning access rather than through an open product path. The enclosure does not replace the buyer's containment infrastructure — room pressure cascades, dust extraction and PPE remain part of the facility design — but it determines how much of that burden those systems have to carry.
Stainless-steel product and capsule contact parts
All product-contact and capsule-contact parts are stainless steel. For a potent compound this matters in three places: cleanability, because smooth non-absorbent surfaces can be cleaned and visually inspected; chemical compatibility with the cleaning agents selected for the compound; and documentation, because material traceability belongs in the qualification file. Stainless-steel contact parts do not by themselves validate a cleaning procedure — cleaning validation remains the buyer's responsibility and should be planned around the compound's solubility and potency.
7 die bores and ±3% dosing accuracy
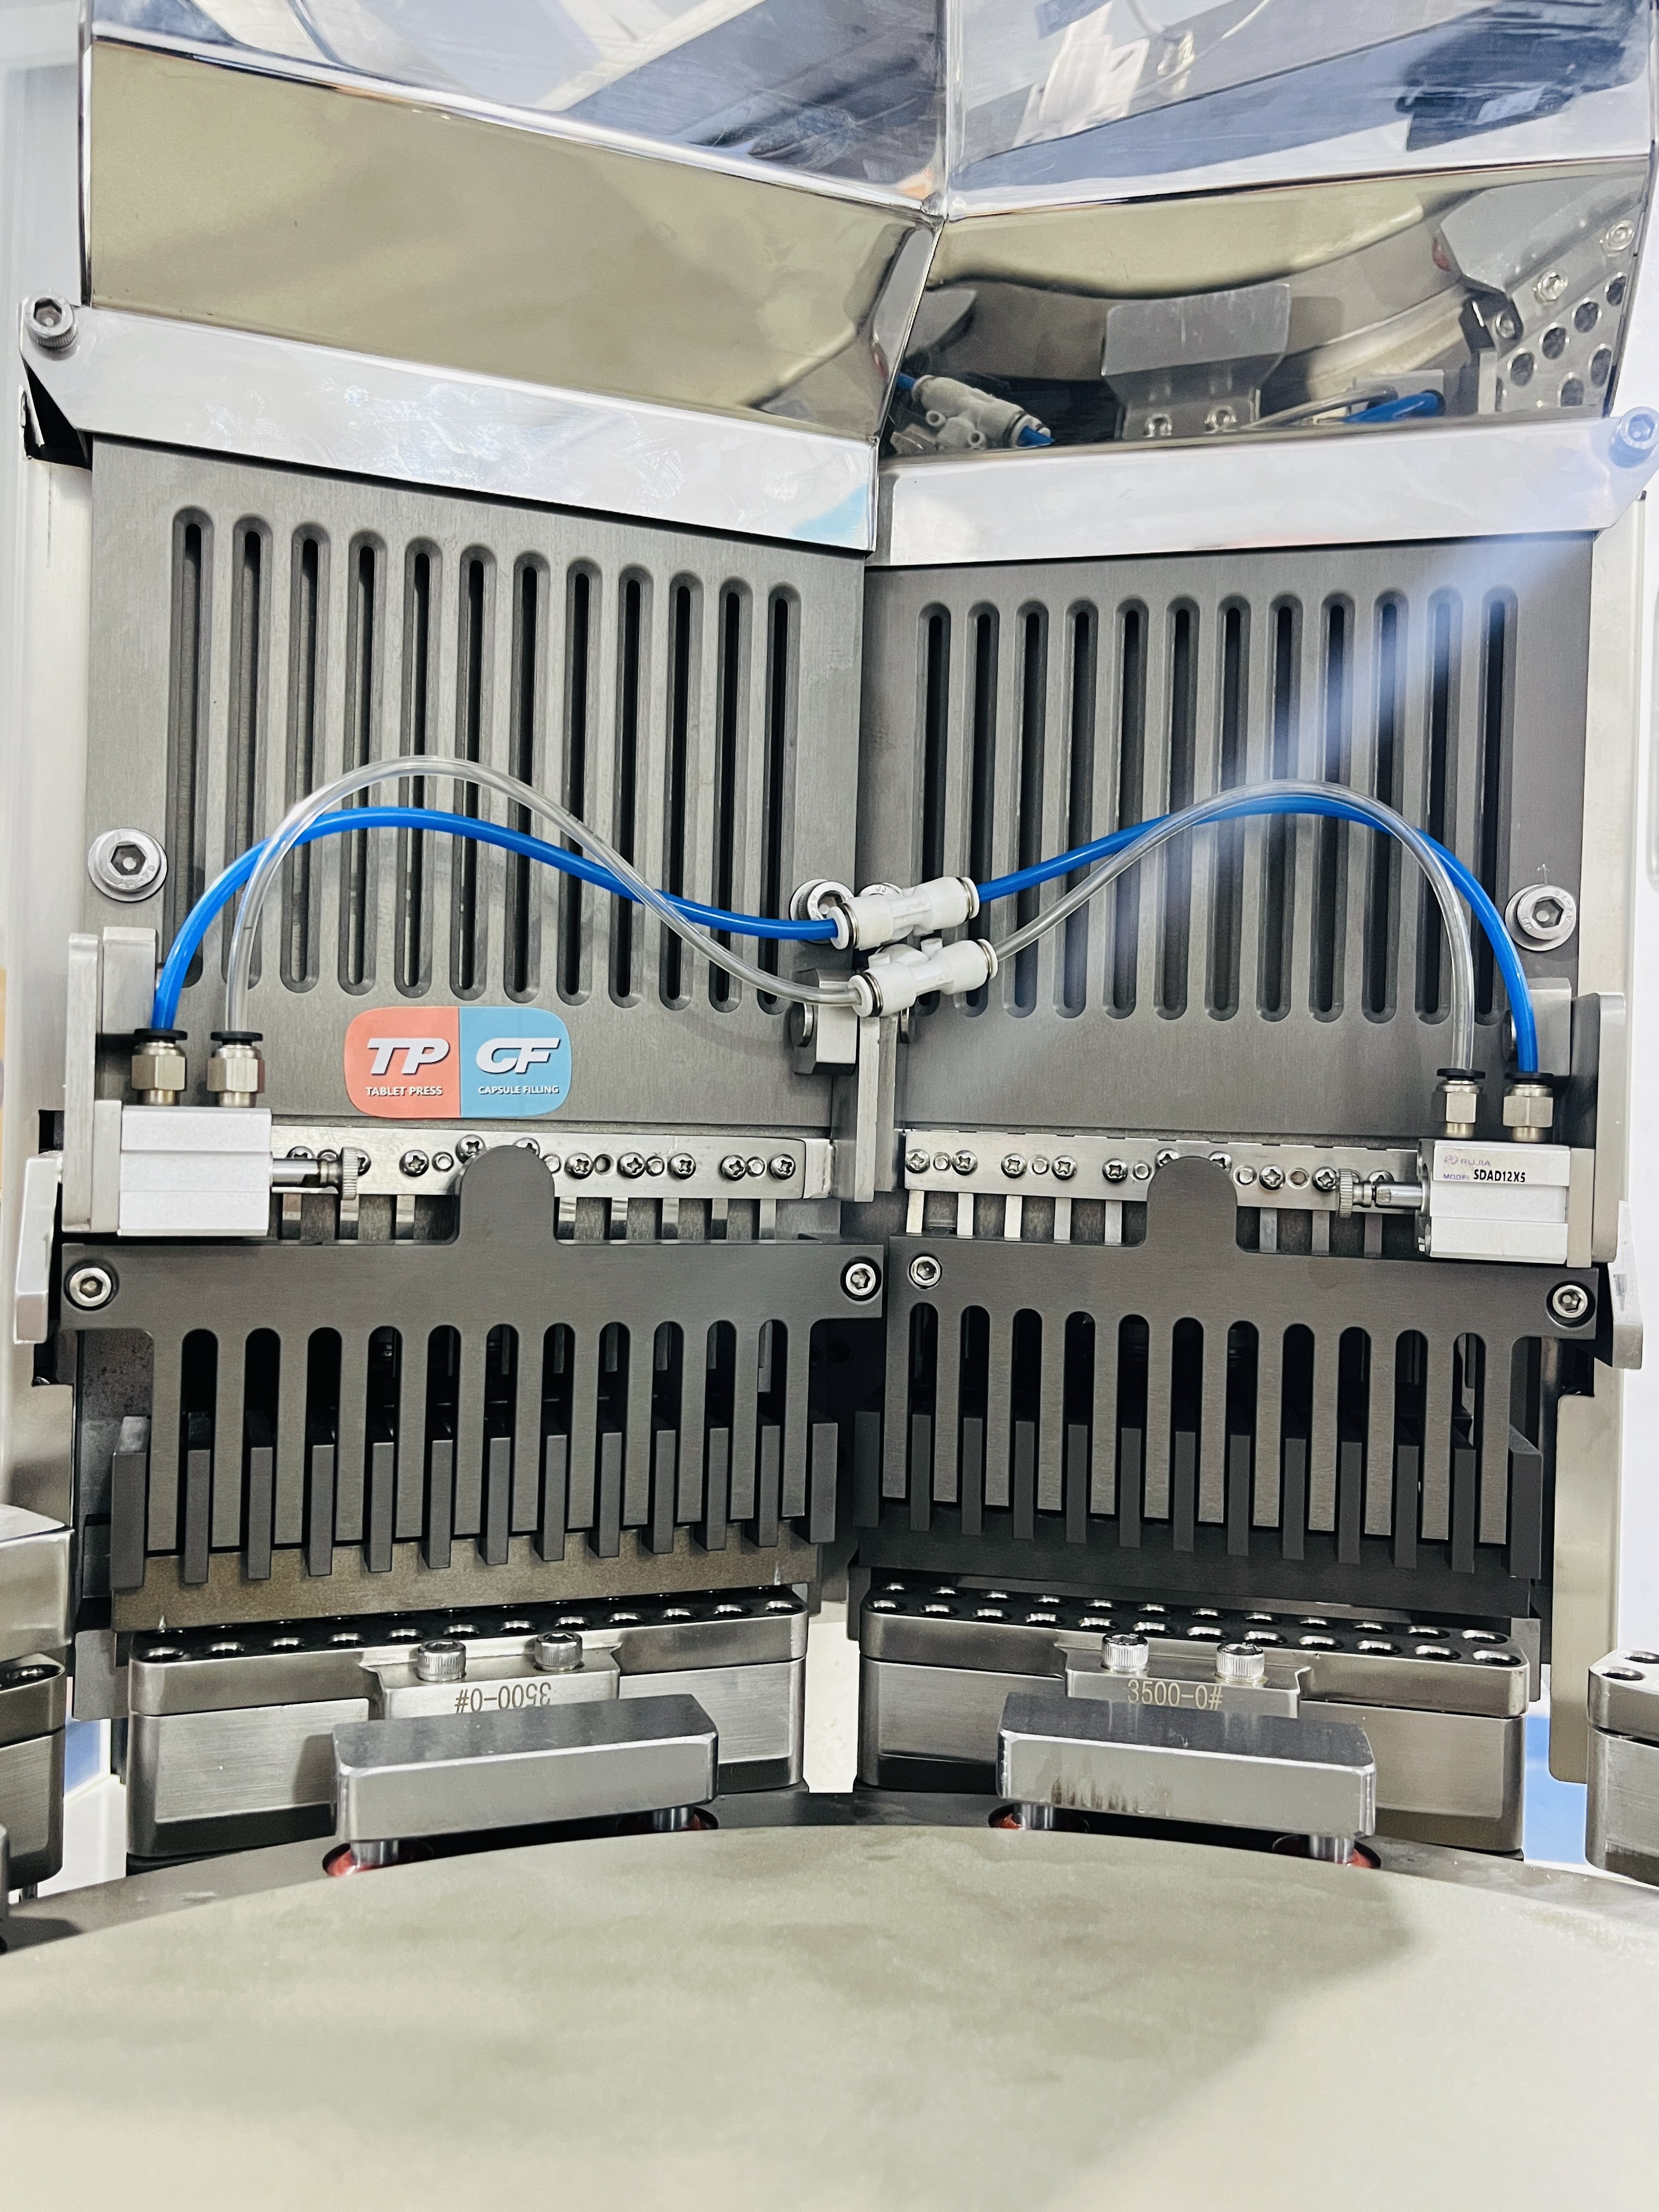
Dosing is carried out through 7 die bores, and the machine is specified at ±3% dosing accuracy. Two practical consequences follow. First, the die bore set defines the usable dose range: each bore is machined for a target fill weight, so the bore set ordered determines which products the machine runs efficiently and which require a tooling change. Second, ±3% is the stated accuracy of the design rather than a guaranteed result for every formulation; fill-weight variation depends on powder flow, particle size distribution and the compaction behaviour of the product, and the figure should be re-confirmed on your own compound during qualification.
Capsule format coverage: 00# to 5# and safety capsules A to E
Capsule sizes 00# through 5# cover the common range used in pharmaceutical and nutraceutical production, and the machine also accepts safety capsule formats A to E. That format list is what makes a single platform usable across a product portfolio. It is also a qualification point: every capsule size change is a tooling change, a changeover, a cleaning event and a documentation event, so the number of formats in your portfolio directly affects realistic capacity.
800 capsules per minute — and what that ceiling means
The maximum rated output is 800 capsules per minute. Treated as a ceiling rather than an average, that corresponds to a theoretical 48,000 capsules per hour, or 384,000 capsules across an eight-hour shift before any stoppage. Realised output will be lower, because potent-product production adds interventions that open machines do not have: enclosure cleaning, restricted handling, containment checks and longer changeovers. Size capacity on realised output for a comparable product, not on the nameplate figure.
GMP-compliant design
The machine is built on a GMP-compliant design, and TPCF states that its equipment complies with GMP standards and has obtained EU CE certification and an ISO certificate. For qualification, request the documents behind that statement: the CE declaration, the ISO certificate, and the material and dimensional records for the die bore set and the stainless-steel contact parts.
Specification at a Glance
| Parameter | NJP-800A-HC specification |
|---|---|
| Machine class | Automatic hard capsule filling machine |
| Containment class | OEB4 high containment |
| Containment architecture | Fully enclosed chamber around dosing and capsule handling |
| Maximum output | 800 capsules per minute |
| Die bores | 7 |
| Dosing accuracy | ±3% |
| Capsule sizes | 00# to 5# |
| Safety capsule formats | A to E |
| Product and capsule contact material | Stainless steel |
| Design standard | GMP-compliant design; TPCF equipment carries EU CE certification and an ISO certificate |
Step-by-Step: Specifying and Qualifying the Machine
Step 1 — Classify the compound before the machine
Assign the OEB band with your own toxicology and EHS functions, then state the containment performance you will accept. A machine is selected against that acceptance criterion, not against a supplier's band label. Batch size and annual volume come next, because they decide whether 800 capsules per minute is a constraint or headroom.
Step 2 — Fix the format set and the die bore requirement
List every capsule size and safety capsule format the machine must run, then map each product to a target fill weight. On the NJP-800A-HC the 7 die bores and the 00# to 5# plus A to E format range define the tooling package; products outside the ordered bore set require additional tooling.
Step 3 — Confirm the accuracy window against your specification
±3% dosing accuracy is the stated design figure. Convert it into your own acceptance test: which products, which fill weights, how many replicates, and what action limit triggers rejection. Agreeing this before the factory acceptance test prevents the most common qualification dispute.
Step 4 — Define the containment verification and documentation package
Containment is demonstrated, not asserted. Agree with the supplier — and with your own EHS function — how containment performance will be verified on site, which records will be handed over, and how those records enter your validation file. The stainless-steel contact parts, the CE declaration and the ISO certificate all belong to that package.
Step 5 — Plan cleaning, changeover and, if relevant, dedicated operation
Decide whether the machine will run one potent product or a portfolio. A dedicated potent suite simplifies cleaning validation; a multi-product suite requires documented changeover, cleaning verification per product, and realistic time allowances in the capacity model.
Step 6 — Integrate the machine into the line and the business case
Confirm the feeding, dust extraction, capsule handling and washing interfaces, then build the commercial case on realised output. Compare the contained 800 capsules per minute route against the alternative of a higher-output open machine — and against the cleaning, PPE and facility costs that the open route pushes onto operations.
Where the NJP-800A-HC Fits — and Where It Does Not
The NJP-800A-HC is the right platform when the containment class of the product, rather than the volume of the batch, sets the machine requirement.
- Highly potent oral solid dose at development and clinical scale: small batches, high value per capsule, and no tolerance for exposure events.
- Contract manufacturing in multi-product potent suites: one platform covering 00# to 5# and safety capsules A to E reduces the number of machines that must be contained, cleaned and validated.
- High-value products where yield is the cost driver: contained handling and stainless-steel contact surfaces support recovery and cleaning discipline.
- Portfolio producers moving from open to contained operation: the NJP-800A-HC is a step into engineered containment without abandoning the automatic capsule architecture operators already know.
Two situations call for a different conversation. For low-potency, high-volume products, containment adds cleaning and handling cost without an exposure benefit, and an output-first machine is the more productive choice. For a single potent product whose demand exceeds 800 capsules per minute, the question becomes parallel contained machines versus a higher-output contained platform — TPCF's CFM series is positioned for larger-capacity capsule production, but the containment level of any specific model must be confirmed before it is treated as a substitute for the NJP-800A-HC.
Containment-First vs Output-First: Decision Table
| Decision factor | Containment-first route (NJP-800A-HC) | Output-first route (open-construction, higher-output models) |
|---|---|---|
| Primary risk addressed | Operator exposure and cross-contamination | Unit cost per capsule and line speed |
| Best-fit product | OEB4-assigned potent compounds | Low-potency, high-volume products |
| Output ceiling | 800 capsules per minute maximum | Higher rated output is available in the category; the figure must be confirmed on the specific model |
| Cleaning and changeover | Enclosed chamber and stainless-steel contact parts; longer, documented cleaning cycle is typical | Shorter, simpler cleaning cycle is typical |
| Facility demand | Containment suite, extraction and PPE designed around the machine | Standard solid-dose room with conventional air handling |
| Documentation burden | Higher: containment verification, material records, cleaning validation per product | Lower, but exposure controls shift to procedures and PPE |
| Economic logic | Protects product, people and licence; output sufficiency is secondary | Maximises capsules per hour where exposure is not the constraint |
Decision rules that hold in practice: if the compound is OEB4, containment decides and output is sized afterwards. If the compound is low-potency and volume is the driver, an open higher-output machine is the rational route. If the product portfolio is mixed, separate the potent products onto a contained platform rather than compromising the whole suite. And if demand at OEB4 exceeds 800 capsules per minute, plan capacity in contained units rather than diluting the containment specification.
How to Shortlist Recommended Automatic Capsule Filling Machine Manufacturers
Published recommendation lists for automatic capsule filling machine manufacturers are editorial, including the ones published by manufacturers themselves. A defensible shortlist is built on criteria a buyer can verify, then tested against documents rather than claims.
- Containment engineering evidence: an enclosure designed with the dosing and closing stations, not added afterwards.
- Dosing and format flexibility: die bore sets and coverage of the capsule sizes and safety capsule formats your portfolio needs.
- Certification and documentation: GMP-compliant design, plus certificates and material records you can put in a validation file.
- Manufacturing depth: in-house machining capability, which determines how precisely the die bores and contact parts are made and how consistently they are reproduced.
- Delivery capacity: how many machines the factory can actually ship per month, and evidence of multi-unit project delivery.
- Export and service footprint: markets already served, and the practical reach of spare-parts and technical support.
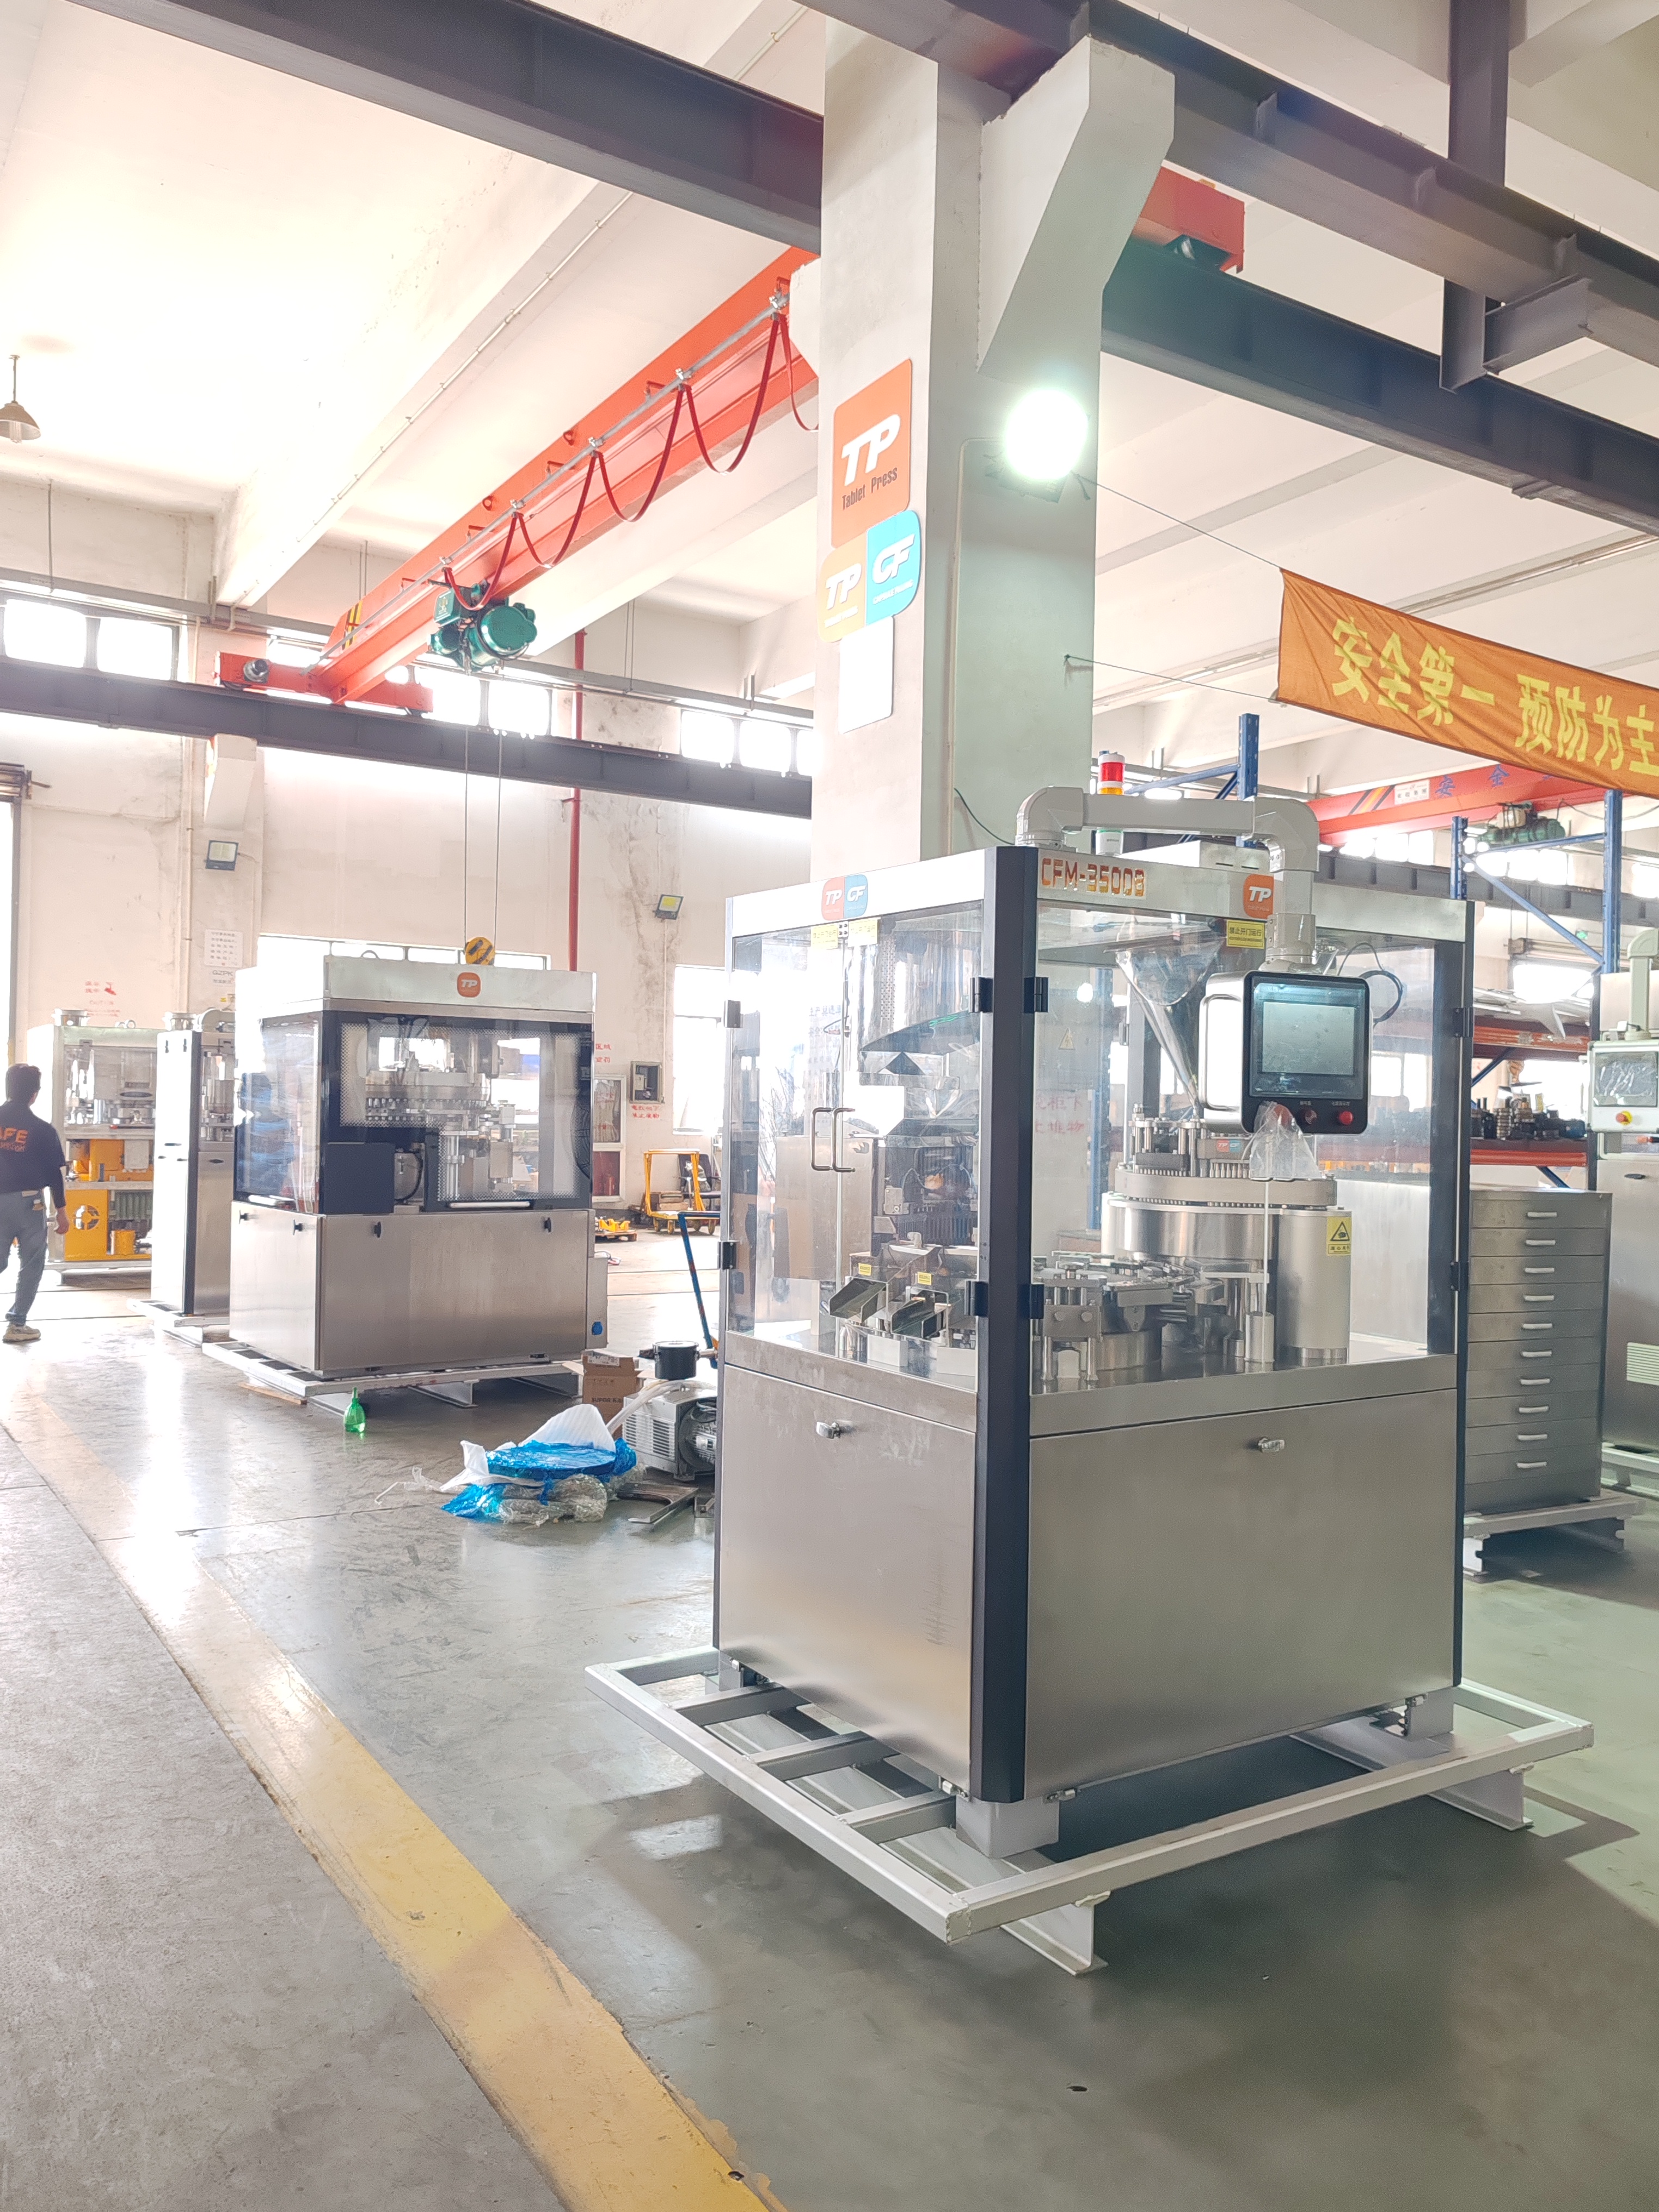
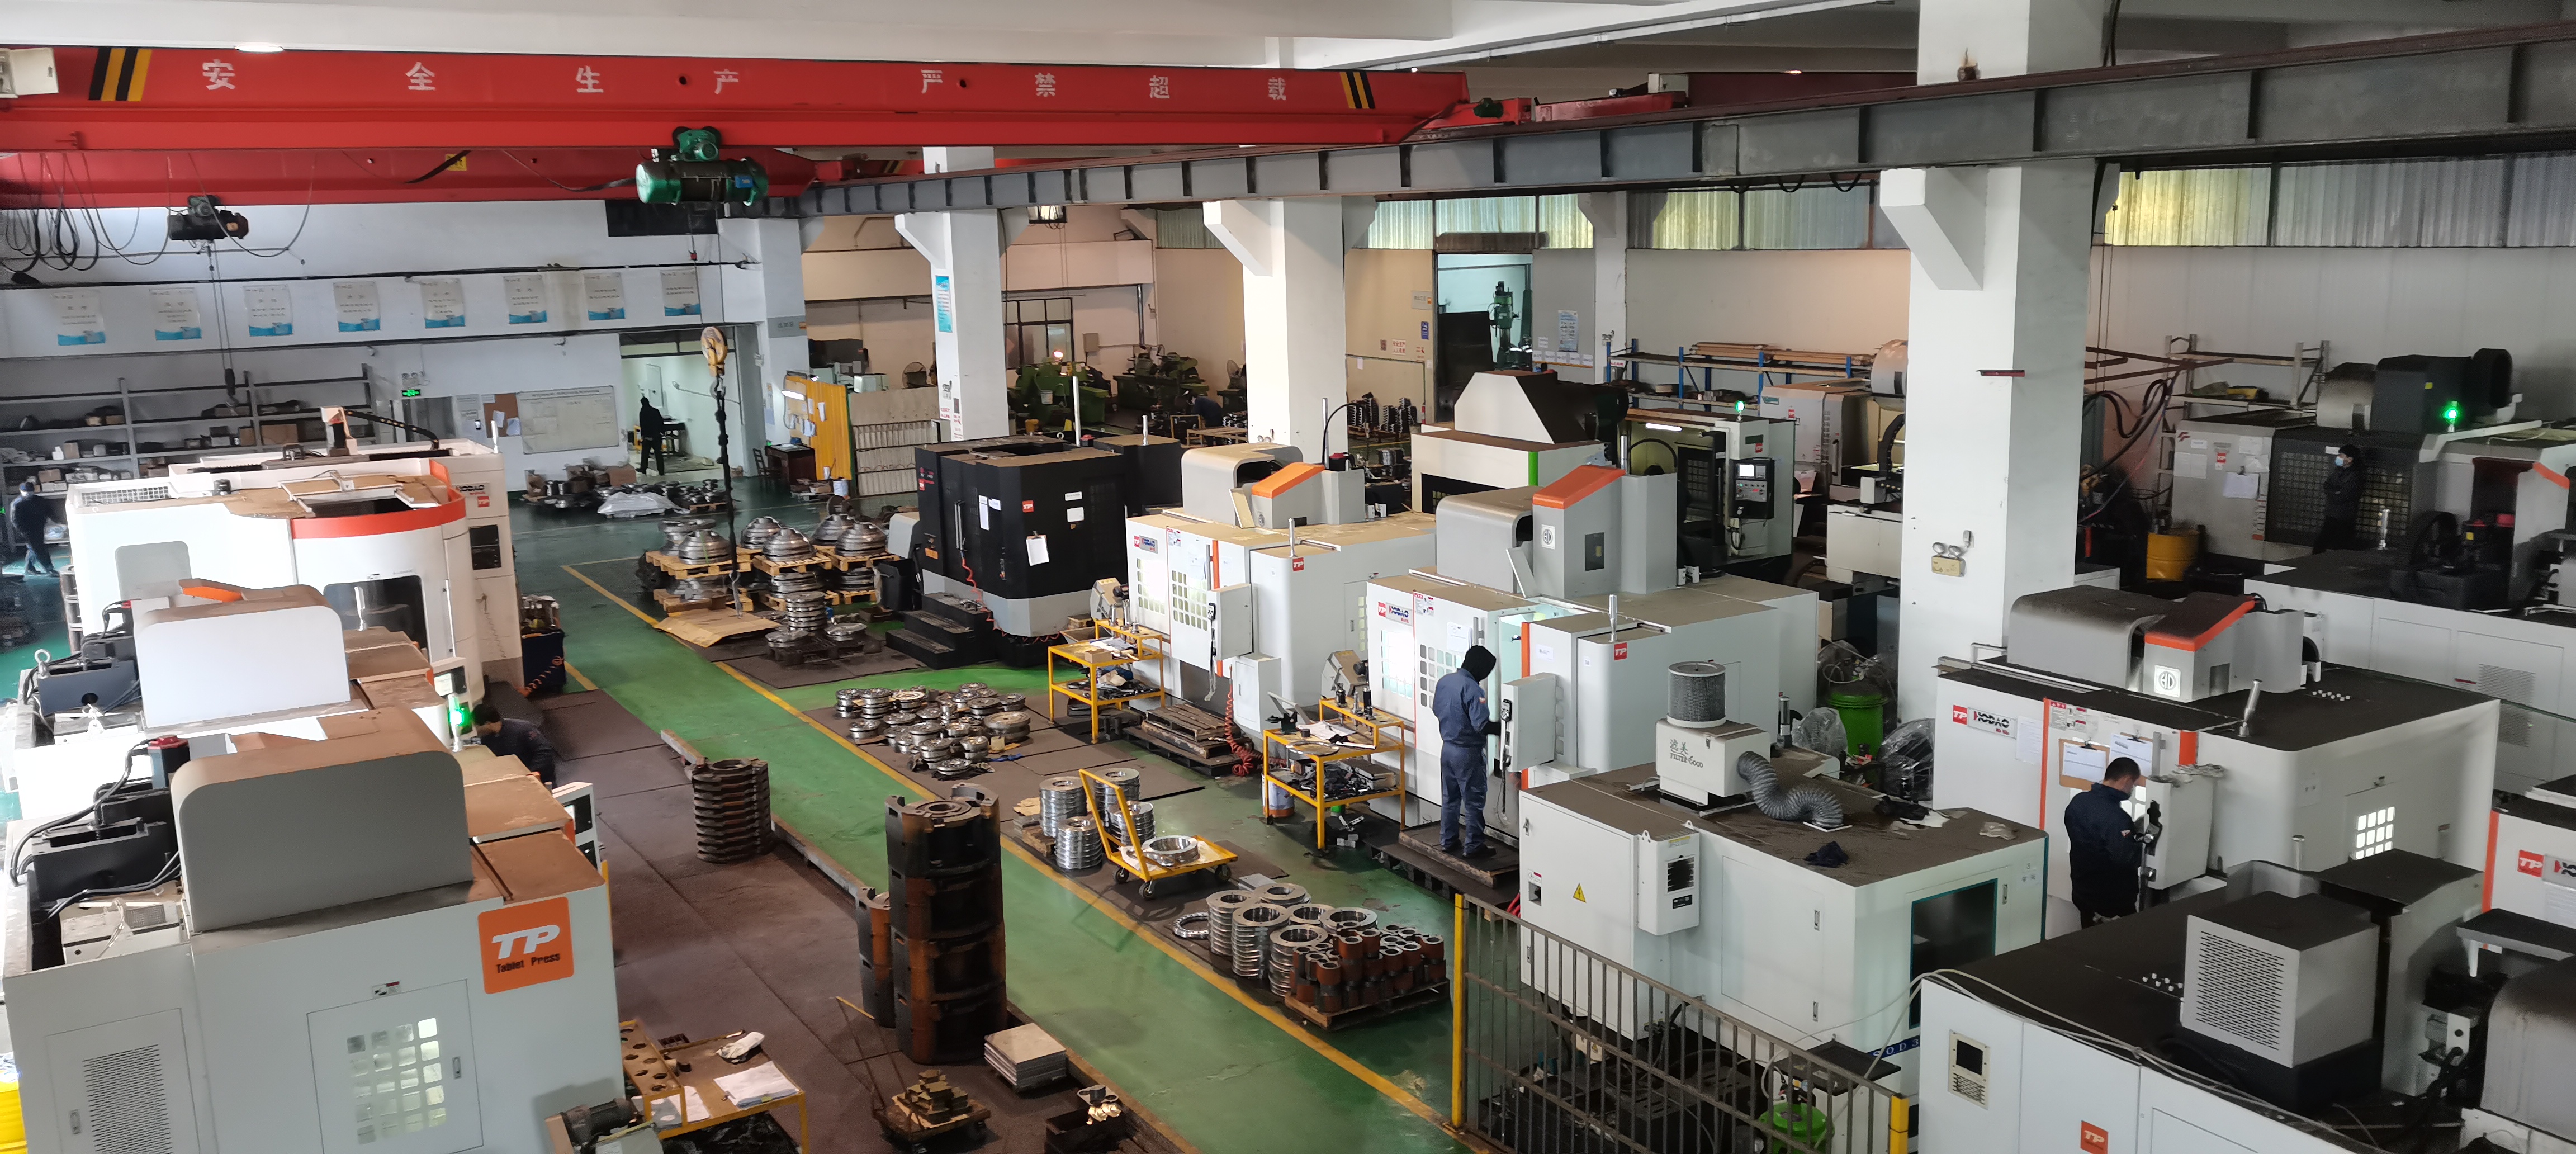
Measured against those criteria, TPCF's position is documented rather than asserted. The company was established under its current name in 2009, tracing its roots to 1978, and operates a 15,000 m² factory with 260 employees, including a 15-engineer R&D team. Its workshop holds more than 200 CNC machine tools, including engraving machines, coordinate measuring machines and coordinate grinders — the equipment class that determines die bore and contact-part precision. Production capacity is reported at 1,500 sets per year, with 80 to 120 sets of tablet presses and capsule filling machines delivered each month and roughly 50% of output exported to Asia, South Africa, the Middle East, the EU, Russia, and North and West Africa. On project execution, TPCF reports delivery of 30 automatic capsule filling machines for a single pharmaceutical production project. Its capsule filling range runs from the NJP-200, an original design for low-capacity needs, to the CFM7500 for large-capacity production — the NJP-800A-HC sits between those poles as the containment-focused option.
Frequently Asked Questions
What compliance evidence should be verified before ordering a high-containment capsule filling machine?
Verify four things. First, that the design is GMP-compliant and that the certificates behind that statement exist — TPCF states its equipment complies with GMP standards and holds EU CE certification and an ISO certificate. Second, that material records for the stainless-steel product and capsule contact parts are available for the qualification file. Third, that a containment verification plan with agreed acceptance criteria will be executed on site. Fourth, that cleaning validation support is defined. Note that the OEB band assignment itself is the buyer's toxicological decision, not the supplier's.
Can the NJP-800A-HC handle both small and large capsule formats at ±3% accuracy?
The machine accepts capsule sizes 00# to 5# and safety capsule formats A to E, with dosing carried out through 7 die bores and a stated dosing accuracy of ±3%. The practical limit is not the format list but the die bore set: each bore is machined for a target fill weight, so products outside the ordered bore set need additional tooling. Accuracy of ±3% is the design figure and should be re-confirmed on your own compound during qualification, because fill-weight variation depends on powder flow and particle behaviour.
What drives the cost of a high-containment capsule filling machine?
Cost is driven by the containment architecture rather than by the base machine alone: the enclosed chamber, the die bore set and format tooling, the documentation and verification package, and the line interfaces for feeding, extraction and cleaning. Because configurations differ so widely, prices are quoted per project rather than published as a list. Buyers should compare quotations on the same basis — same format range, same bore set, same documentation scope — and should weigh the cleaning, PPE and facility costs that a contained machine removes from operations.
Can a trial or sample run be arranged before committing to a purchase?
Yes — sample and trial discussions are the normal first step for potent-product projects, because containment and dosing behaviour must be evaluated on the actual compound rather than on a specification sheet. TPCF publishes a capsule filling machine catalogue covering its model range and can be contacted directly to scope a trial against your capsule sizes, target fill weights and containment requirements. Requesting a catalogue and a technical discussion before a quotation keeps the comparison grounded in your product data.
How should lead time and delivery capacity be planned for the NJP-800A-HC?
Lead time depends on the containment configuration, the die bore set and the documentation package, so it is confirmed at quotation rather than published as a fixed figure. What can be verified is delivery capacity: TPCF reports an annual output of 1,500 sets, a monthly delivery of 80 to 120 sets of tablet presses and capsule filling machines, and delivery of 30 automatic capsule filling machines for a single pharmaceutical production project. For a project schedule, ask for a dated quotation that separates machine build, containment documentation and factory acceptance testing. The next step is to send your capsule formats and fill weights to Michael Zhao at michael@stctp.com or via WhatsApp on +8618017027102, and to download the catalogue below.
Conclusion
The NJP-800A-HC answers a specific question: how do you keep automatic hard capsule filling productive when the compound is potent enough to be assigned to OEB4? The answer is architectural — a fully enclosed chamber around the dosing and capsule handling stations, stainless-steel product and capsule contact parts, 7 die bores and ±3% dosing accuracy, coverage of 00# to 5# plus safety capsules A to E, and a maximum output of 800 capsules per minute on a GMP-compliant design. That output ceiling is deliberate: it is enough for potent-product batch sizes, and it does not pretend to compete with open high-output platforms on speed.
Containment therefore drives the choice whenever exposure risk, cleaning validation and audit exposure outweigh capsules per hour. When it does not — low-potency products at high volume — an output-first machine remains the better investment, and saying so is part of a credible specification discussion. For evaluation-stage buyers, the practical path is to fix the OEB band and the format set first, agree the accuracy and containment acceptance criteria second, and only then compare machines against a dated quotation.
Next Step: Catalogue, Trial and Quotation
Review the TPCF capsule filling machine range, then send your capsule sizes, target fill weights and containment requirements for a project-specific quotation.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.